When we retrofit 3-roll bending machines at shipyards across Asia, the first question operators ask isn't about force capacity or diameter range—it's about eliminating the pre-bend pass. That single pain point explains why asymmetrical 3-roll configurations now dominate new installations at EZHONG's production facilities.
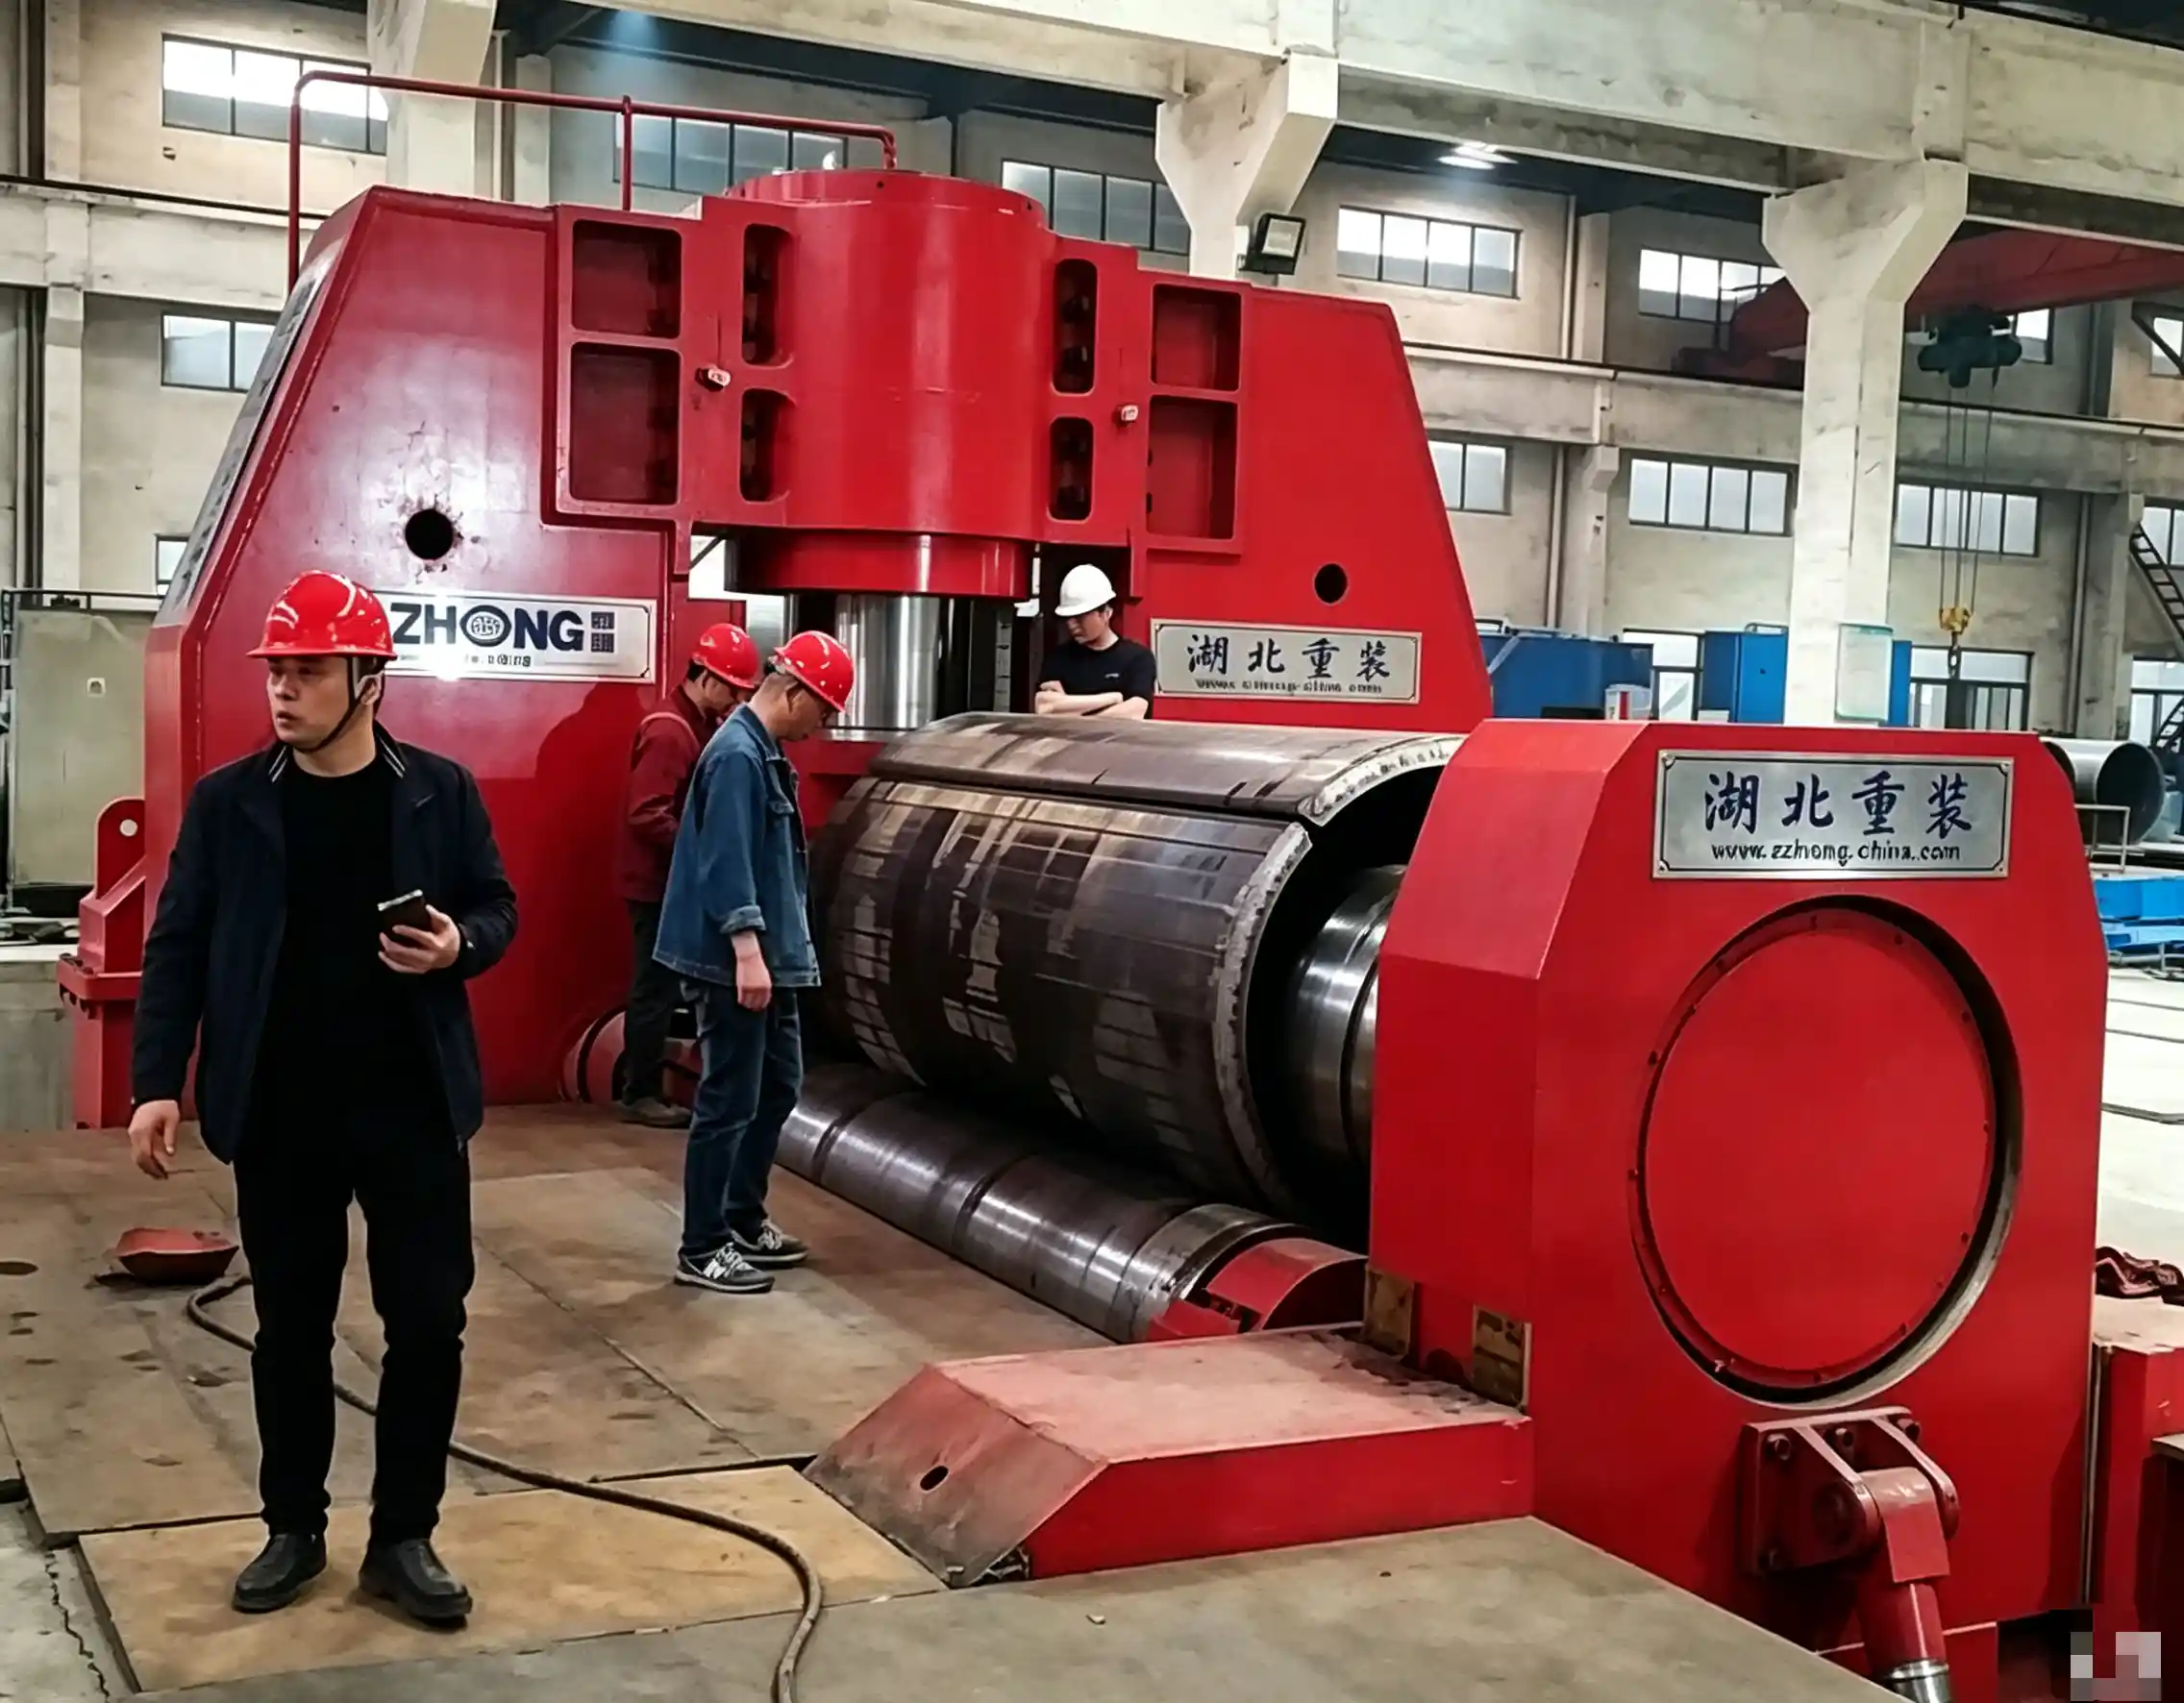 Asymmetrical 3-roll plate bending machine in industrial workshop
The difference comes down to roller geometry. In a symmetrical 3-roll machine, both lower rollers sit equidistant from the center axis. The upper roller descends between them, forcing the plate into an arc through three-point bending.
Asymmetrical designs shift one lower roller closer to the feed side. This creates an offset geometry where the plate enters at a steeper attack angle. The result: initial bending happens on first contact, not after the plate fully engages all three rollers.
Here's what that geometry change delivers on the shop floor:
| Parameter | Symmetrical 3-Roll | Asymmetrical 3-Roll |
|---|---|---|
| Pre-bending Required | Manual or auxiliary press | Integrated single-pass |
| Flat End Length | 2.5× plate thickness | 0.8× plate thickness |
| Setup Time (12m cylinder) | 45-60 minutes | 20-30 minutes |
| Scrap Rate (thin gauge) | 4-7% | 1-3% |
| Operator Skill Level | Certified journeyman | Intermediate (6 months) |
At a pressure vessel manufacturer we work with in Jiangsu, switching from symmetrical to asymmetrical 3-roll machines cut their wind tower production cycle time by 32%. The gains weren't from rolling speed—that stayed nearly identical—but from eliminating the pre-bend station entirely.
Traditional symmetrical machines require pre-bending both plate ends before rolling. On a 50mm thick, 12-meter plate, that's two separate press operations, two crane moves, and two quality checks. Each adds 15-20 minutes and introduces alignment risk.
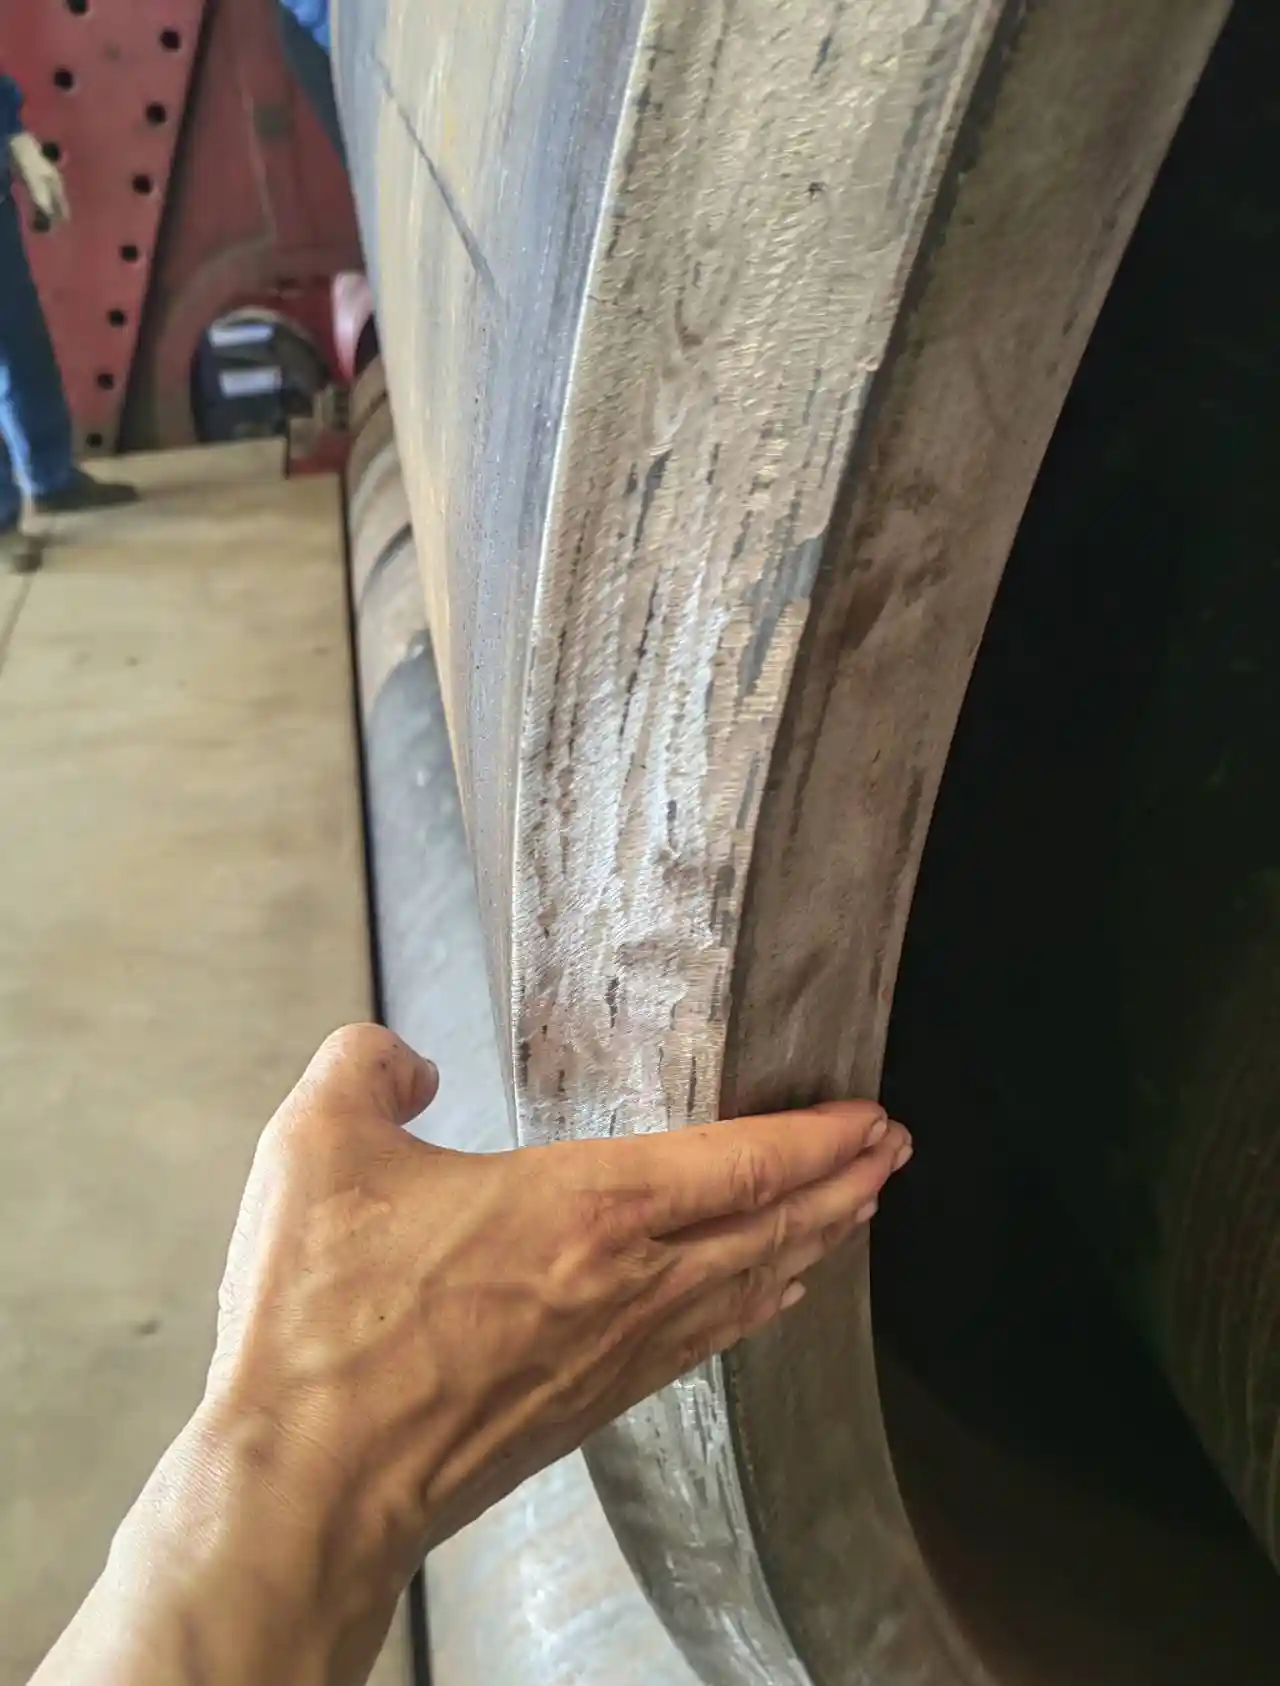 Pre-bending operation on symmetrical plate rolling machine
Asymmetrical machines handle initial bending during the first rotation. The offset lower roller creates sufficient wrap angle that the leading edge forms correctly without auxiliary equipment. For shops running single-shift operations, this saves 2-3 hours daily across multiple parts.
But asymmetrical isn't universally superior. When forming pressure vessel shells above 80mm thickness, we've documented higher springback variation with asymmetrical geometry compared to 4-roll machines.
The issue traces to roller deflection. In asymmetrical setups, the offset lower roller bears asymmetric loading. On thick plates, this creates differential deflection that varies across the plate width. The result manifests as cylindricity errors—typically 3-5mm on a 4-meter diameter vessel with 100mm wall thickness.
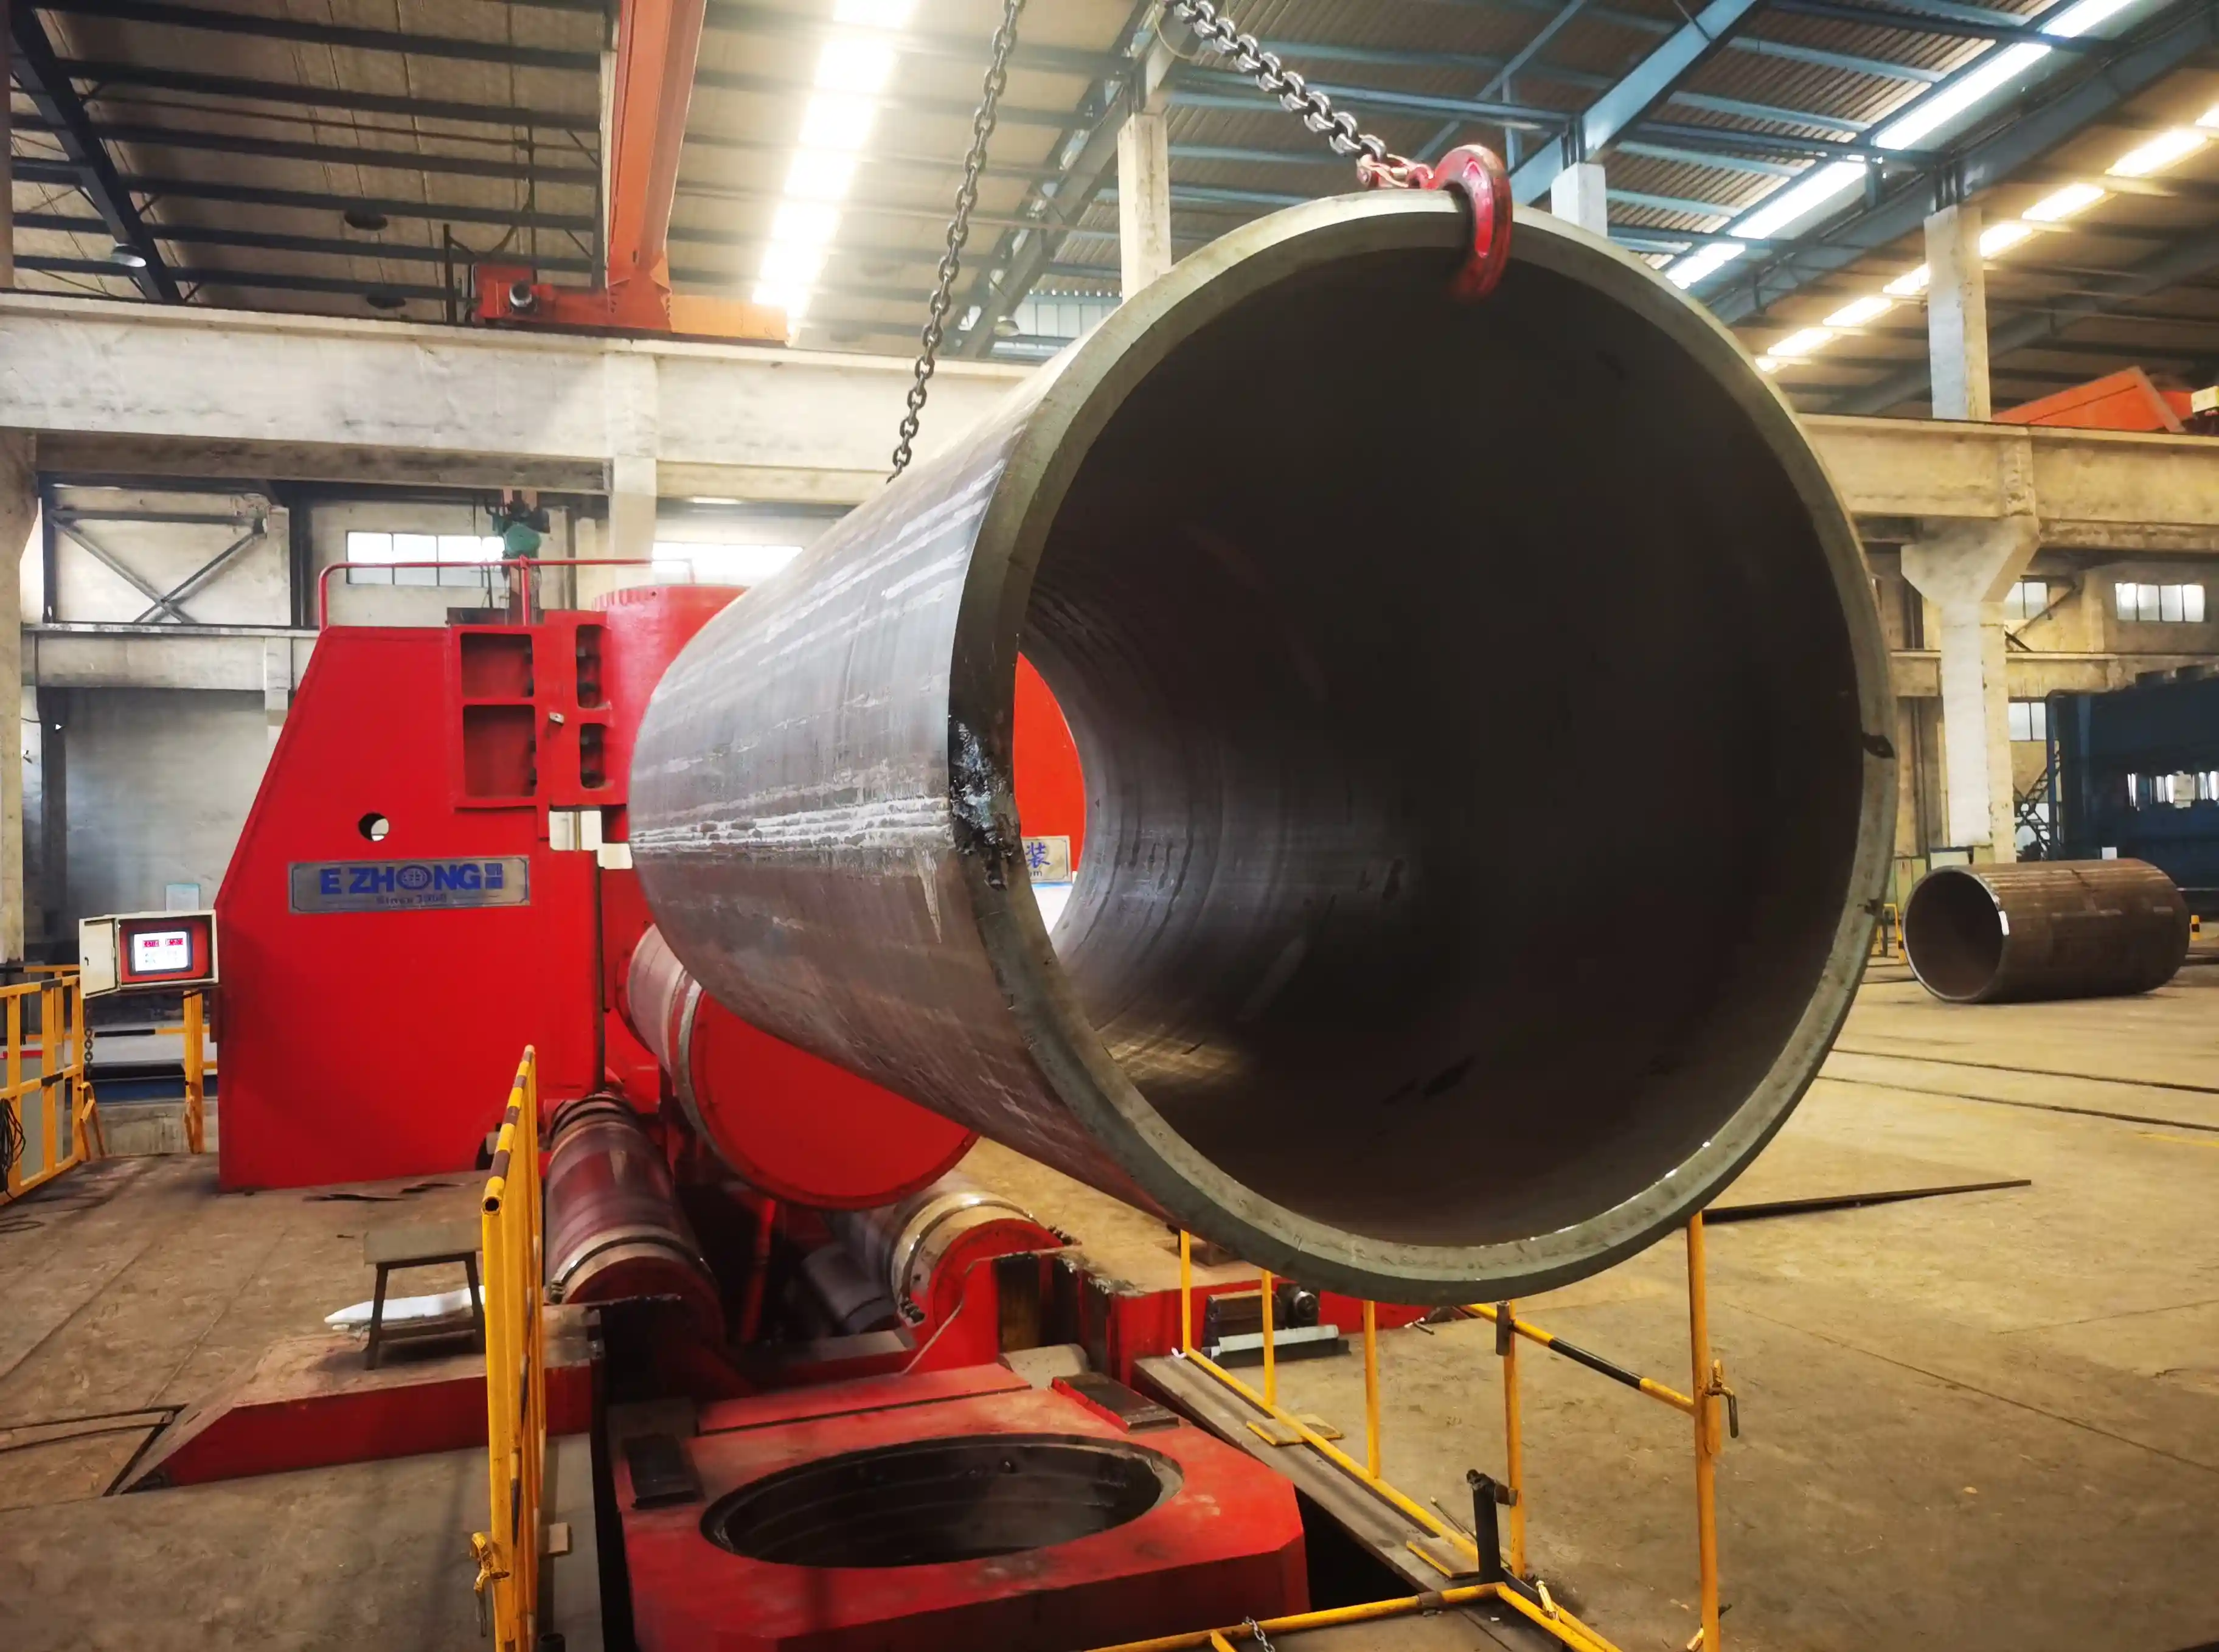 Thick plate pressure vessel shell being formed on plate rolling machine
Symmetrical 3-roll machines distribute forces more evenly, but they can't match the pre-bending capability of a true 4-roll configuration with independent side rollers. That's why 4-roll CNC machines remain the standard for ASME Section VIII work requiring ±2mm tolerance.
The mechanical geometry gets attention, but control architecture determines whether an asymmetrical machine delivers its theoretical advantage. We've commissioned both CNC and manual asymmetrical machines—the performance gap is wider than between symmetrical and asymmetrical manual units.
CNC Control Advantages:
Manual machines require operator interpretation at every adjustment. An experienced roller can match CNC results on repetitive jobs, but setup time doubles and consistency suffers when switching materials.
High-strength steel above 960 MPa introduces complications with asymmetrical geometry. The offset roller configuration creates non-uniform stress distribution during forming. With materials that work-harden significantly (like QT steel or AR plate), this can produce varying mechanical properties across the cross-section.
We documented this on a ship plate rolling project using 1100 MPa steel. Tensile tests showed 8% hardness variation between the feed side and trailing edge after forming. A symmetrical machine on the same material produced 3% variation.
For mild steel and standard structural grades, this isn't measurable. But in applications where post-form mechanical properties matter—pressure vessels, offshore structures, seismic components—it's a specification risk.
| Selection Factor | Choose Asymmetrical 3-Roll | Choose Symmetrical 3-Roll | Choose 4-Roll |
|---|---|---|---|
| Primary Work | Wind towers, general tanks, pipe < 80mm | Long seam work, custom diameters | Pressure vessels, thick wall, tight tolerance |
| Thickness Range | 8-60mm optimal | 6-80mm | 10-200mm |
| Production Volume | Medium to high (>15 cylinders/week) | Low to medium | Medium to high |
| Tolerance Requirement | ±3-5mm cylindricity | ±5-8mm cylindricity | ±1-2mm cylindricity |
| Floor Space | 12-15m length typical | 12-15m length typical | 15-18m length + pre-bend access |
| Investment Level | $$ | $ | $$$ |
EZHONG's latest S-series machines use adjustable lower roller positioning. Operators can shift between symmetrical and asymmetrical geometry by moving the feed-side roller along a guideway. This adds mechanical complexity but provides setup flexibility for shops that run diverse work.
The trade-off is in the adjustment mechanism itself. Each geometry change requires stopping production, repositioning, and recalibration—typically 30-45 minutes. It works for job shops that switch between wind tower cones and large-diameter pipes, but it's inefficient for dedicated production lines.
Time studies from our customer installations show where asymmetrical machines actually save time:
Symmetrical 3-Roll Setup (60mm × 3000mm plate to 2500mm diameter):
Asymmetrical 3-Roll Setup (same part):
The 32-minute difference compounds across shifts. On a three-cylinder-per-day production schedule, that's 96 minutes recovered—essentially a full extra part per week.
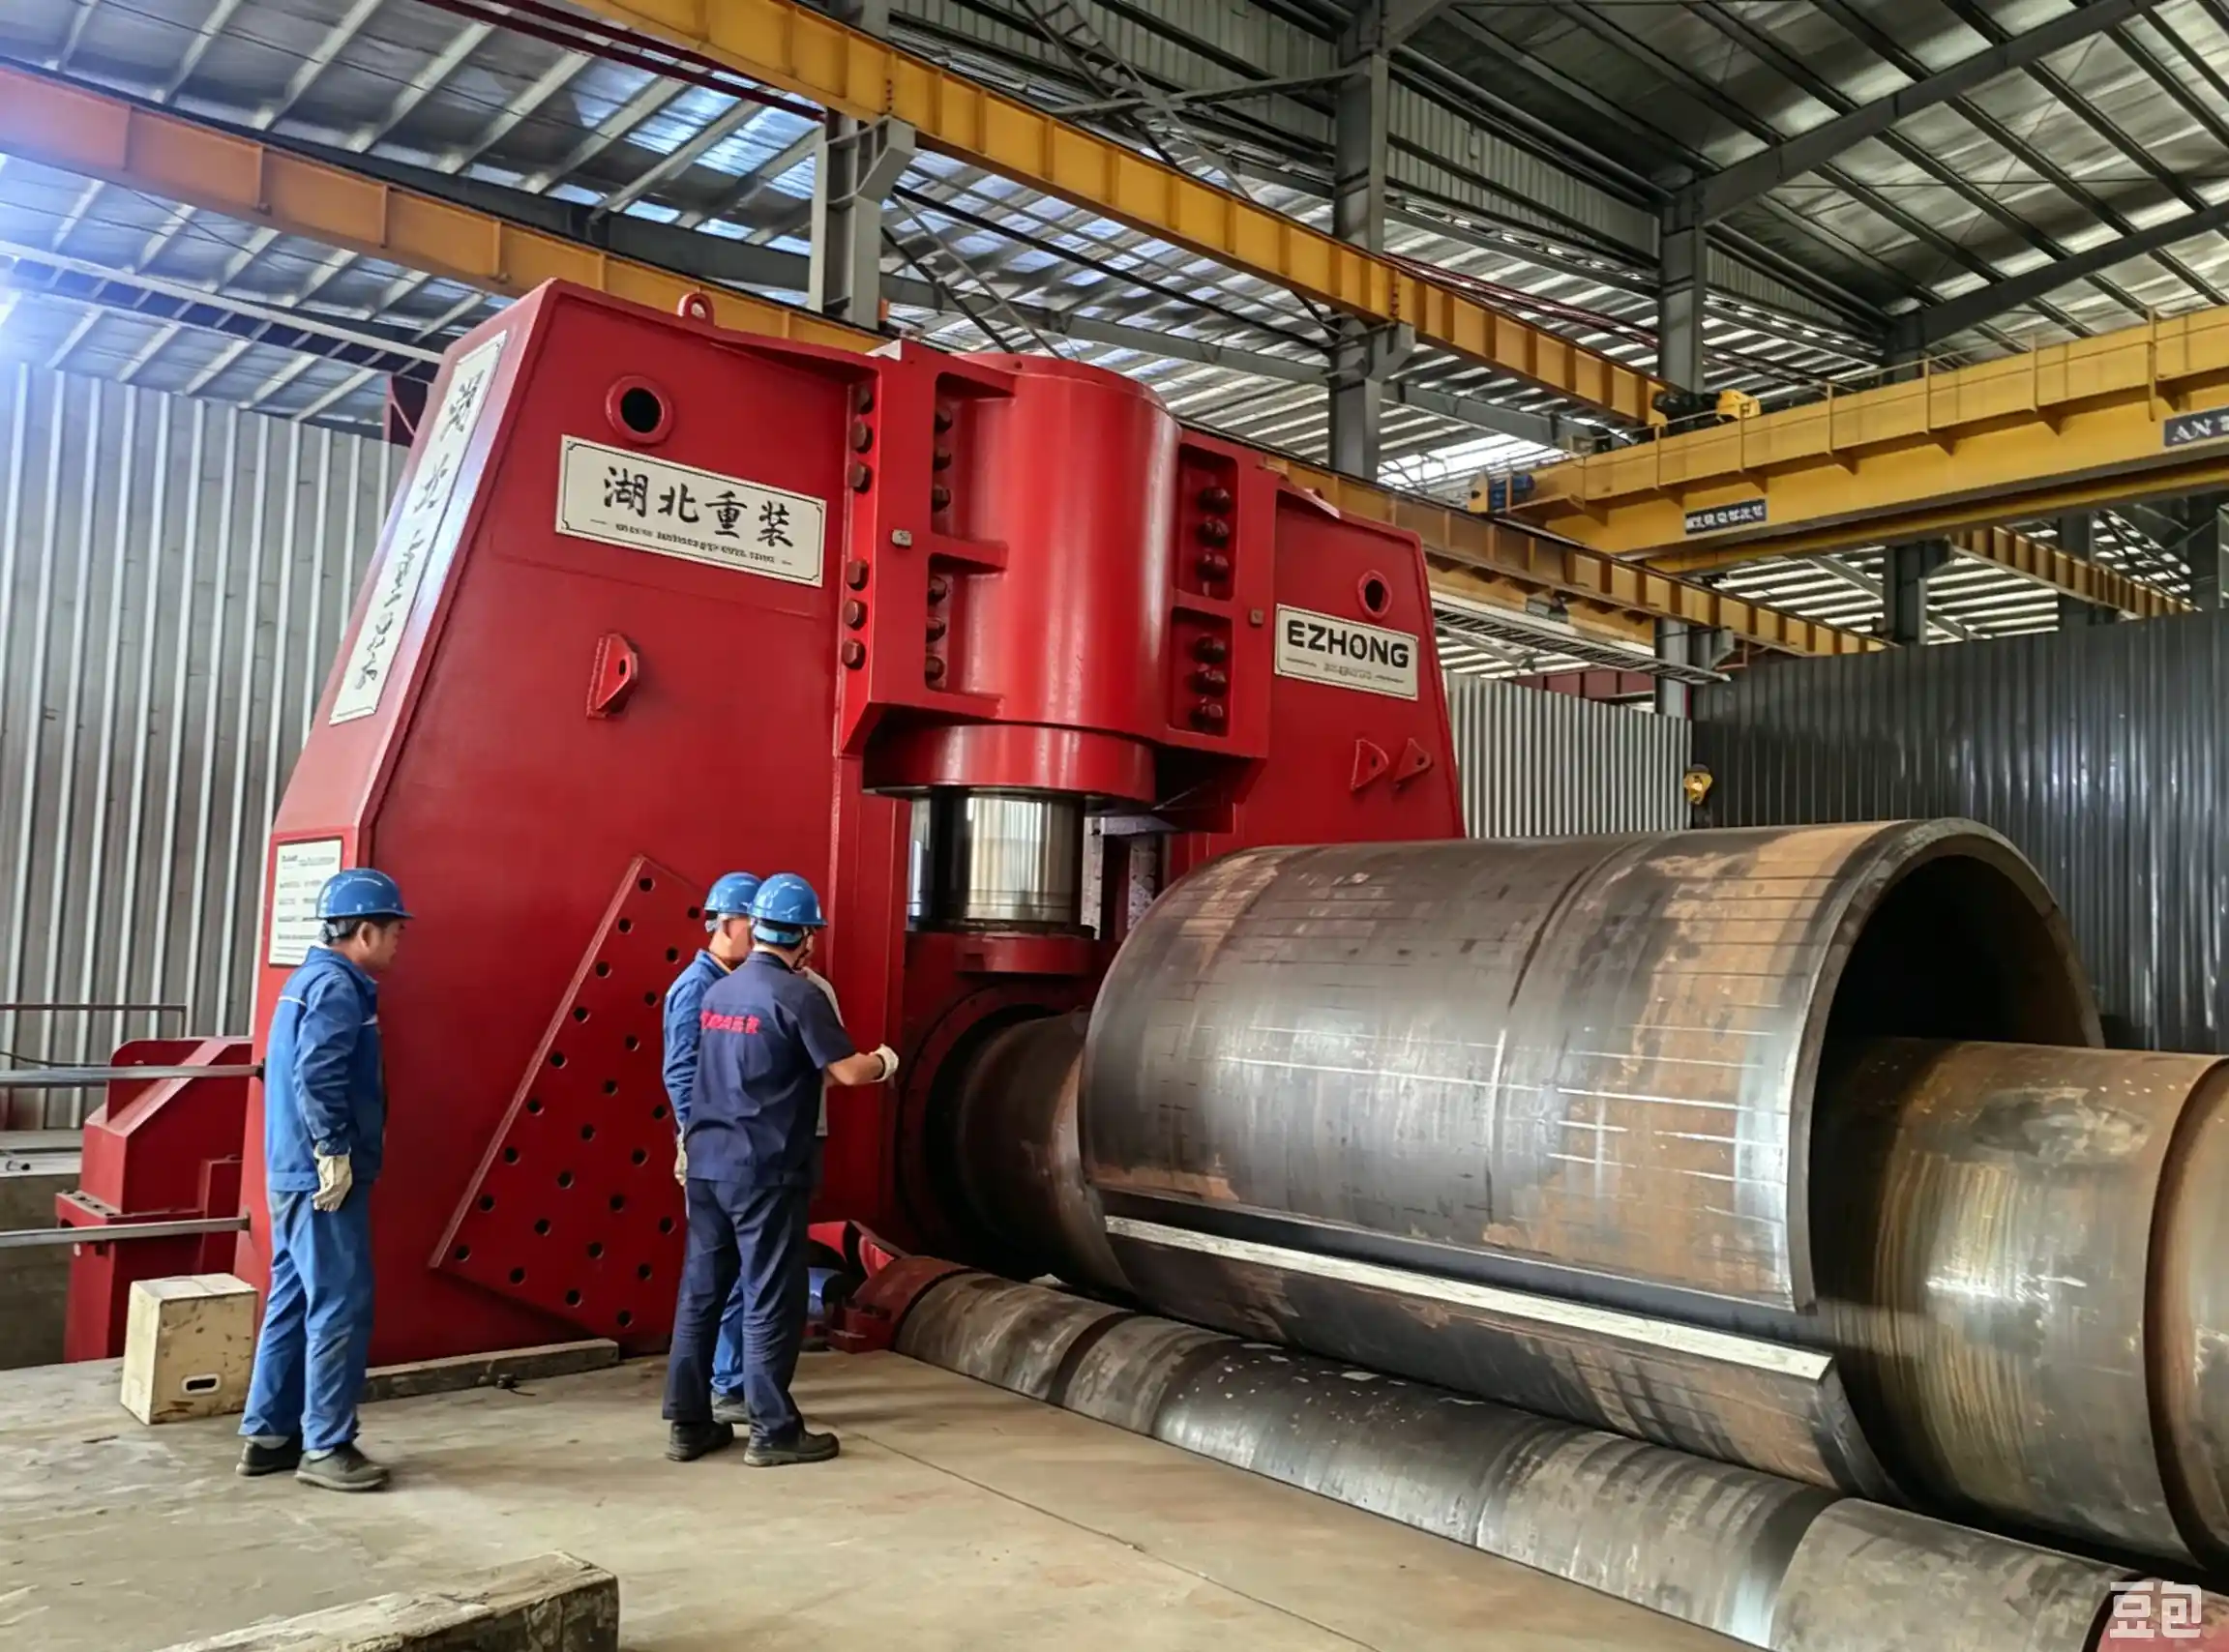 Completed cylindrical shells from plate rolling machine undergoing quality inspection
After servicing hundreds of 3-roll machines, bearing failure patterns differ between configurations. Asymmetrical machines show accelerated wear on the offset lower roller bearing—typically 20-30% shorter service intervals compared to symmetrical designs.
The asymmetric loading creates higher radial forces on one bearing assembly. We recommend 1500-hour inspection intervals for asymmetrical machines versus 2000 hours for symmetrical units. This isn't a design flaw—it's physics. Budget for it in your total cost of ownership.
Asymmetrical 3-roll machines excel in a specific production envelope: moderate thickness, good volume, standard tolerances. Outside that envelope, other configurations make more sense.
Stay with symmetrical 3-roll if:
Move to 4-roll if:
Q: Can asymmetrical 3-roll machines handle conical shapes?
A: Yes, but with more setup complexity than 4-roll machines. You'll need to adjust roller angles between passes, which reduces the setup time advantage. For dedicated cone production (wind tower sections), specialized cone rolling machines deliver better results.
Q: What's the minimum diameter an asymmetrical machine can form?
A: Practical limit is typically 1.2-1.5× the distance between lower rollers. For a machine with 600mm roller spacing, minimum diameter is around 800-900mm. Going smaller requires different roller configurations or a different machine type.
Q: How does plate width capacity compare between symmetrical and asymmetrical designs?
A: Width capacity depends on roller length and frame rigidity, not the symmetry of roller positioning. Both configurations can handle identical width ranges when built on the same frame platform.
Q: Is the learning curve steeper for operators moving from symmetrical to asymmetrical?
A: Actually easier. The reduced pre-bending requirement simplifies the process. Operators typically reach competency 30-40% faster on asymmetrical machines because there are fewer steps to master.
Q: Can I retrofit my existing symmetrical 3-roll to asymmetrical geometry?
A: Theoretically yes, but rarely cost-effective. You'd need to modify the frame, reposition bearing housings, and potentially upgrade the control system. The engineering and downtime costs usually exceed 60-70% of a new machine price.
Asymmetrical 3-roll plate bending machines deliver measurable productivity gains in moderate-thickness, mid-to-high-volume applications. The elimination of separate pre-bending operations cuts setup time by 30-60% for typical cylindrical work between 20-60mm thickness.
But they're not universal solutions. Thick-wall forming above 80mm, ultra-tight tolerances, and high-strength materials still favor symmetrical 3-roll or 4-roll configurations. The key is matching machine geometry to your actual production requirements, not chasing the latest design trend.
At EZHONG, we've installed both configurations across industries from shipbuilding to steel pipe manufacturing. The decision comes down to three factors: your typical thickness range, required tolerance level, and production volume. When those align with asymmetrical advantages—specifically 15-60mm thickness, ±3-5mm tolerance, and batch production—the ROI is clear and fast.
For shops outside that envelope, symmetrical 3-roll or 4-roll machines remain the better investment. Match the tool to the work, not the marketing.